Turnkey projects
Turnkey Food Processing Lines: From Product Trials to Commissioning
What a turnkey food processing project includes: supply levels, product trials, layout and interfaces, FAT and SAT, installation, training and hand-over.
- Prepared by
- HNFODA Applications Engineering
- Topic
- Turnkey projects
- Published
- Reading time
- 5 min read · 2 sources
On this page
- 01Five supply levels
- 02Step 1: Product trials and process validation
- 03Step 2: Layout and interfaces
- 04Step 3: Manufacturing and factory acceptance test (FAT)
- 05Step 4: Installation, commissioning and training
- 06Step 5: Site acceptance test (SAT)
- 07Who is responsible for what
- 08What you receive at hand-over
- 09Planning a plant?
Short answer: A turnkey food processing line is a project in which one supplier takes responsibility for the process line from an agreed start point to an agreed end point: product trials, layout, equipment, line controls, installation, commissioning, training and acceptance. It works when the interfaces are written down: what HNFODA supplies, what the buyer provides (building, utilities, permits, food safety validation), and which figures the line must reach at the site acceptance test.
HNFODA has designed and manufactured food processing machinery since 2010 and exports to more than 80 countries. We support customers through manufacturing, installation and the warranty period. This page explains how a turnkey project is set up, so you can decide which level of supply you need and prepare the right information.
Five supply levels
You do not have to buy a full turnkey project. Choose the level that matches your team and your site.
| Supply level | What we quote | What must be agreed |
|---|---|---|
| Single machine | Main machine, specified tooling or contact parts, electrical control, manuals, agreed spare parts | Feeding and discharge method, connection heights, power supply, cleaning method, safety guards |
| Section | Several machines, conveying and controls within the section, buffers where needed | Start and end points of the section, buffer time, interlocks with upstream and downstream equipment, maximum variation in flow |
| Complete line | Process layout, equipment list, line controls, test run and hand-over | Whether packing, freezing, cleaning systems, wastewater and utility stations are included, item by item |
| Site services | Installation supervision or installation, commissioning, training, acceptance | Who does the construction work, lifting equipment, utilities ready, trial material, local staff |
| After-sales service | Spare parts, inspections, remote support, on-site repair | Service period, response time, consumables and travel costs, software and data access |
Step 1: Product trials and process validation
Every project for a new product starts with trials. Using representative raw material, trials fix the equipment route, the process window (temperatures, times, speeds, moisture) and the figures that will later be used for acceptance.
Trials can be run in three ways:
- Laboratory trials on small samples, to check feasibility.
- Machine trials on a production-size machine, to measure output, yield and quality.
- Small linked-line trials, to check how stations work together.
What makes trials useful is the sample. It should come from the raw material you will actually buy, ideally from more than one batch or season, in a quantity large enough to run the machine properly. Quality and yield targets should be agreed before the trial, not after.
Step 2: Layout and interfaces
Once the route is fixed, we prepare the layout and the interface list. We provide: equipment outlines, infeed and discharge points, energy consumption and connection points, space needed for cleaning and maintenance, and the electrical and signal list.
The buyer provides the building and site conditions, and confirms who builds and accepts the civil works, ventilation and exhaust, drainage, heat source, refrigeration, fire protection and compressed air.
At this stage we also agree how the line is cleaned, how products change over, and what happens to waste, wastewater and waste oil. These questions are cheap to settle on paper and expensive to fix after installation. For hygienic design of equipment and building details, the EHEDG guidelines are a widely used reference.
Step 3: Manufacturing and factory acceptance test (FAT)
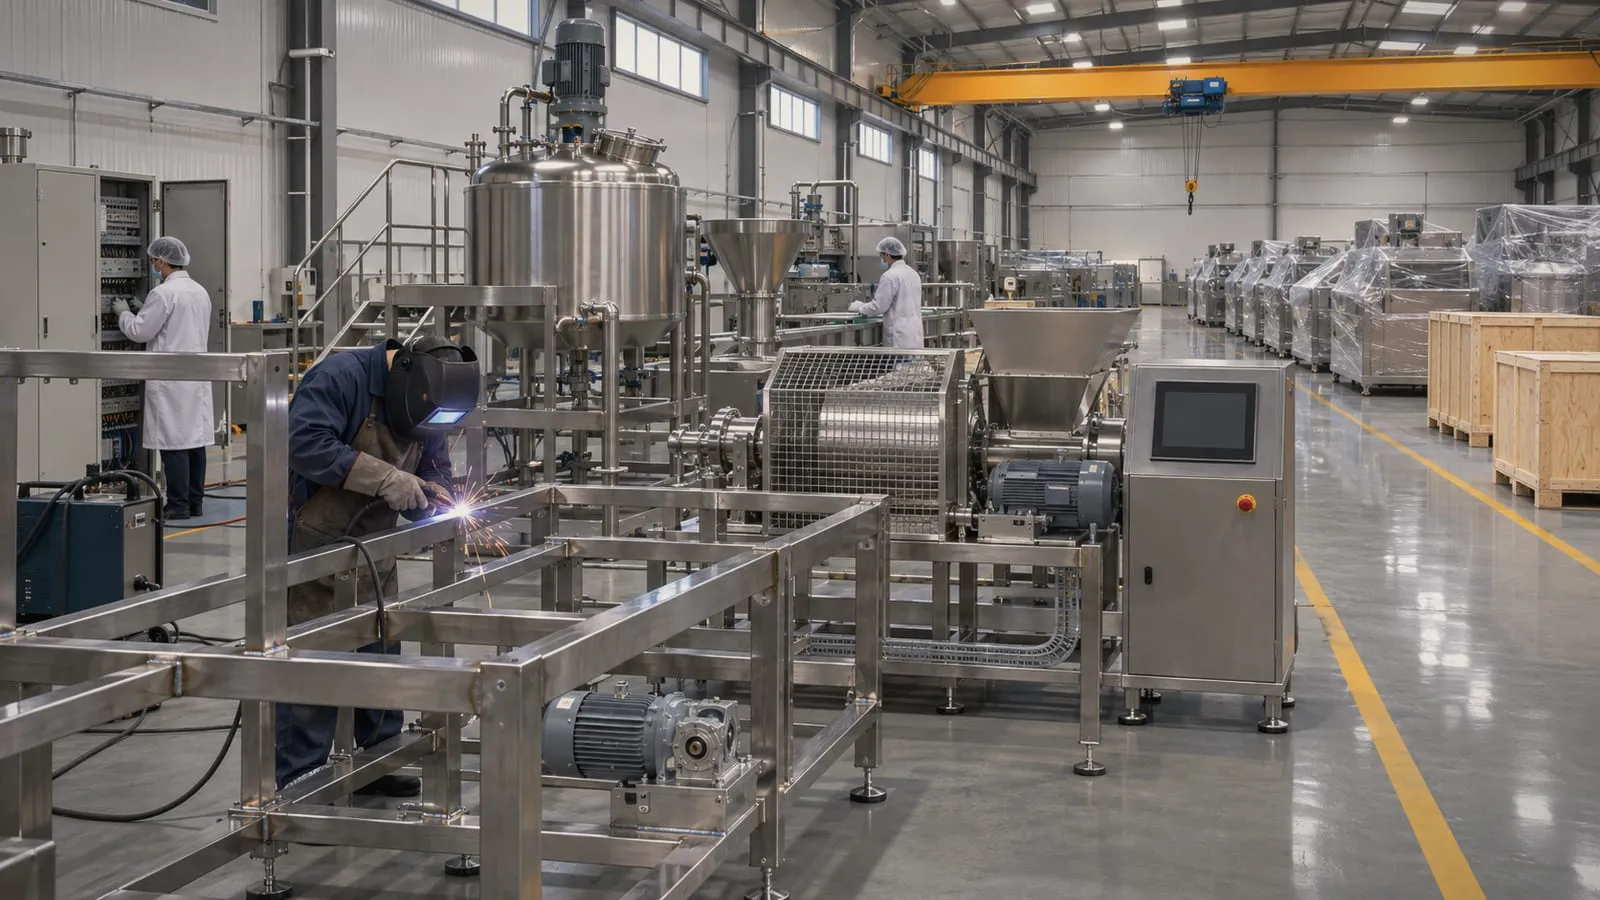
Before shipping, the equipment is assembled and tested at the factory. The FAT checks the agreed movements, interlocks and safety functions, empty running and, where it is practical, a test with material. The buyer or an inspector can attend. Items found at FAT are corrected before the equipment leaves.
FAT cannot prove the line’s real output, because the full line, your raw material and your utilities are not there. That is the job of the SAT.
Step 4: Installation, commissioning and training
On site, the work runs in this order:
- Site readiness check: floors, drainage, power, steam, gas, water and compressed air available at the connection points.
- Installation by our engineers, or by your contractor under our supervision.
- Empty commissioning: each machine, then the line, runs without product.
- Commissioning with product: settings are tuned with real raw material.
- Training for operators, cleaning staff and maintenance technicians, recorded per person.
The buyer usually provides lifting equipment, local labour, trial material and the staff to be trained.
Step 5: Site acceptance test (SAT)
The SAT uses representative raw material and checks the line against figures agreed in the contract:
- Continuous running time
- Net output of good finished product
- Yield
- Finished product specification
- Changeover and cleaning
- How stops and rework are recorded
When the agreed figures are met, the line is handed over.
Who is responsible for what
| Area | HNFODA | Buyer |
|---|---|---|
| Process route and equipment | Proposal, design, manufacture, FAT | Approve route and acceptance figures |
| Building and civil works | Loads, foundations and openings needed | Design, construction and acceptance |
| Utilities | Consumption and connection points | Supply up to the connection points |
| Permits and local approvals | Equipment data needed for applications | Apply for and hold permits |
| Food safety and process validation | Equipment that holds the agreed settings; data for validation | Heat treatment, shelf life and foreign body validation; ongoing monitoring |
| Installation and commissioning | As agreed: install or supervise | Site access, lifting, local labour, trial material |
Heat treatment, sterilisation, shelf life and foreign body detection are validated for each product and pack. The contract states who does the process work, the site validation, the records and the ongoing monitoring. Food safety plans, such as those required by the FDA preventive controls rule in the United States, belong to the food company.
What you receive at hand-over
- Equipment list and wear parts list
- Layout and electrical drawings
- Electrical and software deliverables as agreed
- Operating, cleaning and maintenance manuals
- FAT, commissioning and SAT records
- Training records
Planning a plant?
Our production line pages explain what each type of plant consists of and what to send us before asking for prices: dried fruit, roasted nuts, nut butter, edible oil, instant noodles, frozen dumplings, ready meals and biscuits and snacks. When you contact us, tell us the finished product, target output, raw material and the site you have, and we will suggest which supply level fits.
Frequently asked questions
- What does turnkey mean in your projects?
- It means we take responsibility for the process line from an agreed start point to an agreed end point: layout, equipment, line controls, installation or installation supervision, commissioning, training and acceptance. The building, utilities up to the connection points, permits and food safety validation remain with the buyer unless agreed otherwise.
- Do I need product trials before ordering?
- For a new product or raw material, yes. Trials with representative samples show which route works, what yield and quality to expect, and what figures can fairly be used at acceptance. For standard products on proven machines, trials may be shorter or replaced by reference data.
- What is the difference between FAT and SAT?
- FAT takes place at the factory before shipping and checks movements, interlocks, empty running and, where possible, a test with material. SAT takes place on your site after installation and checks continuous running with representative raw material against the output, yield and quality figures agreed in the contract.
- Who installs the line?
- Either our engineers install it, or they supervise your contractor. In both cases the buyer usually provides lifting equipment, local labour, utilities at the connection points and access to the site. The split is written into the contract.
- What documents do I receive at hand-over?
- An equipment list, a wear and spare parts list, layout and electrical drawings, software and electrical deliverables as agreed, operating, cleaning and maintenance manuals, trial records and training records.
Sources
- [1]EHEDG guideline catalogue (hygienic design) — European Hygienic Engineering & Design Group
- [2]FSMA Final Rule for Preventive Controls for Human Food — U.S. Food and Drug Administration
HNFODA Applications Engineering
Line design, product trials and commissioning
Engineers who size, build and commission HNFODA food processing lines, writing from the questions buyers ask before a quotation. About HNFODA